One column
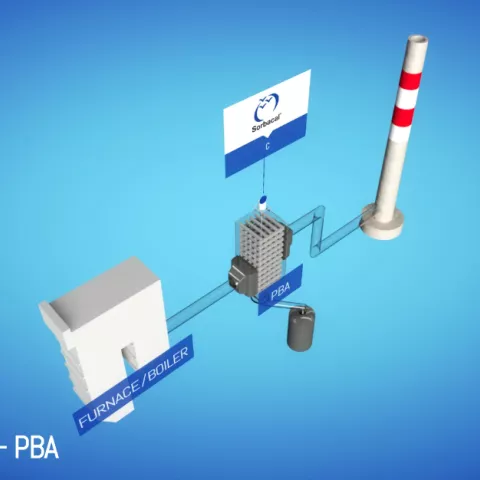
PBA systems treat flue gas by passing it through a fixed bed of granular sorbent, enabling high HF capture in a simple design. Flue gas flows cross‑ or counter‑ current through the bed; pollutants react with the filler, which is replaced once saturated.
Key benefits
- Effective control of peak acidic pollutant releases
- Strong HF and SO3 removal
- Upgradable performance with advanced granulated products
Best-fit applications
Industrial processes with intermittent emission peaks and emerging applications.
Open cta in a new tab
Off
Background Grey
Off
One column
Our Sorbacal® solutions for PBA
Lhoist offers solutions that enhance traditional PBA performance, achieving HCl removal above 70% and SO2 removal up to 35%, or above 80% in multi‑stage PBAs. High performance is achieved particularly with our high‑reactivity Sorbacal® HCG product.
- Sorbacal® C (standard limestone chippings)
- Sorbacal® HCG (granulated CaCO3 + Ca(OH)2)
Open cta in a new tab
Off
Background Grey
Off
Packed Bed Absorber
<notext>
Image
Disable image alteration
Off
https://player.vimeo.com/video/214853830?h=59a29a4a6b&badge=0&autopause=0&player_id=0&app_id=58479
Open cta in a new tab
Off
Small
Image
Disable image alteration
Off
Off
Packed Bed Absorber (PBA)
Market
Route category